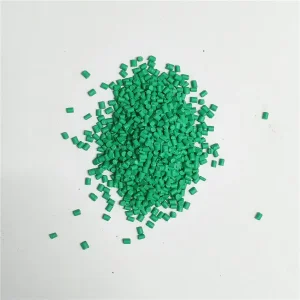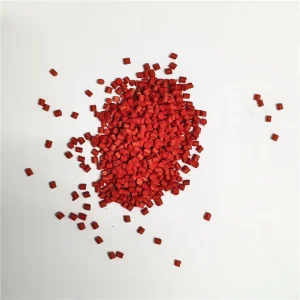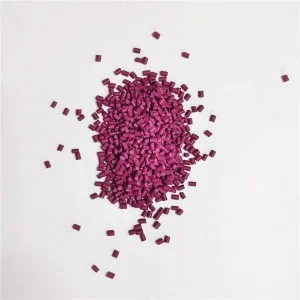
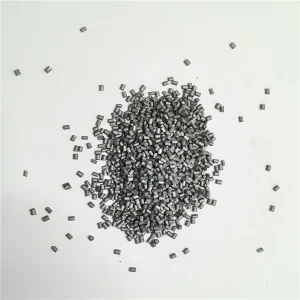
Engineered with sub-micron pigment dispersion, high thermal resistance (up to 260°C), and polymer-carrier compatibility for high-speed automated extrusion lines.
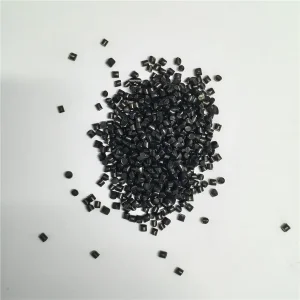
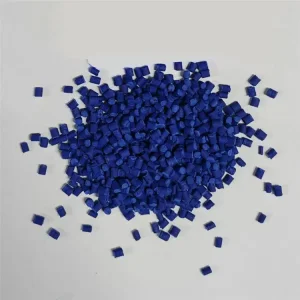
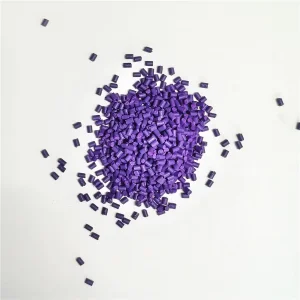
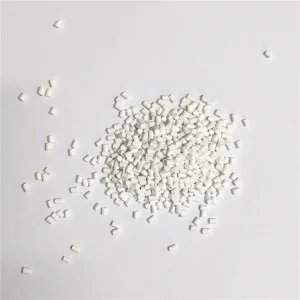
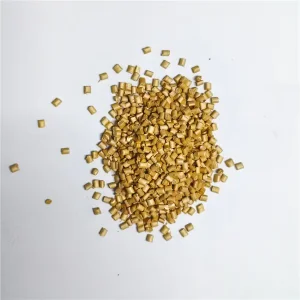
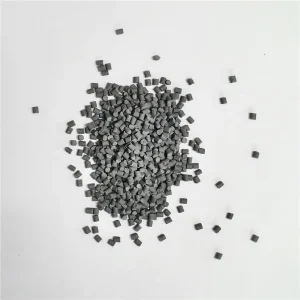
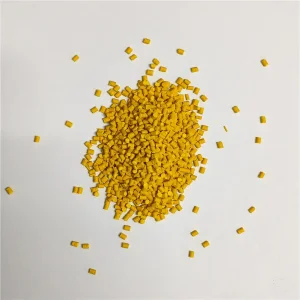
Analyzing the macro-mechanics of high-volume manufacturing: How China's upstream raw chemical integration and automated co-rotating twin-screw compounding create unassailable cost and quality thresholds.
Direct pipeline access to petrochemical majors for linear low-density polyethylene (LLDPE) carriers and ultra-pure rutile titanium dioxide (TiO₂) ensures our raw formulations maintain structural uniformity regardless of global crude fluctuations.
Our Changzhou facility operates multi-zone co-rotating extruders fitted with loss-in-weight gravimetric feeders. This ensures precise shear forces and temperature profiles, breaking down agglomerates to sub-micron particle sizes.
Strategically situated in Jiangsu Province with direct arterial links to Shanghai and Ningbo maritime terminals, we achieve accelerated customs clearing, container optimization, and unbroken cold/dry multi-modal transport lines.
Enterprise buyers do not simply source products; they acquire operational security, formula repeatability, and risk mitigation across complex trans-regional operations.
Global consumer product packaging requires hyper-strict chromatic consistency. Through automated spectrophotometric auditing, our masterbatch ensures minimal spectral variation across multi-ton production campaigns.
High-volume blown film and precision injection molding cannot tolerate unreacted stearates or excessive carrier volatility. We guarantee that colorants do not compromise interfacial polymer shear, corona treatment, or printability.
To hedge against regional shipping disruptions, multinational manufacturers engage Jiazhou as a prime or strategic secondary supplier, locking in annual capacity reservations and stabilizing forward inventories.
Color and filler masterbatches act as functional matrices that directly govern cycle times, mechanical tensile strength, and environmental lifespan.
Micro-dispersion carbon black and UV absorbers prevent pinholing in ultra-thin (down to 8-micron) films while resisting intense chemical degradation from agricultural pesticides and prolonged solar exposure.
Complies with strict OIT (Oxidative Induction Time) protocols. Our black and grey compounds eliminate dielectric stress crack susceptibility and internal pipe wall roughness, securing a verified 50-year service life.
Engineered surface-treated calcium carbonate fillers allow plastic molders to substitute virgin resin up to 30-40% without sacrificing dart-drop impact strength or provoking tear propagation.
Bridging global commercial corridors with ironclad regulatory documentation, traceability, and agile post-sales polymer troubleshooting.
Zero SVHC (Substances of Very High Concern) inclusion. Tested under strict chromatographic spectrometer regimes to comply with EU Directives.
Clean-formulation masterbatches designed for food wrapping, dairy caps, and drinkware packaging complying with FDA Title 21 CFR and EC 1935/2004.
Every super-sack and carton bears serialized batch numbers linked to raw pigment retaining samples held in storage for two full years.
Direct communication with polymer scientists: melt flow rate (MFR) matching, screw RPM adjustments, and thermal stabilization support.
How our ongoing polymer R&D is solving the next generation of industrial environmental mandates, NIR sorting detection, and bio-based carriers.
Pioneering the synthesis of post-consumer recycled (rPE/rPP) based color concentrates that eliminate yellowing degradation, allowing converters to exceed recycled-content regulatory quotas without sacrificing tensile load limits.
Traditional black pigment absorbs Near-Infrared light, rendering containers undetectable in automated recycling plants. Our specialized NIR-detectable formulations solve packaging sorting bottlenecks globally.
Commercializing compostable masterbatches that disintegrate synchronously with aliphatic-aromatic copolyesters, ensuring 100% industrial compostability without leaving heavy-metal pigment traces.
Direct technical and operational answers tailored for corporate sourcing managers, chemical category leads, and global operations directors.
For cataloged color formulations and filler systems, our factory MOQ starts at 500 kg to allow multi-layer line validation. Custom Pantone-matched masterbatches require a 1,000 kg run. Our high-throughput lines maintain a 15-day factory dispatch cycle from deposit and chromatic sign-off.
We deploy DataColor spectrophotometers linked to our automated dosing systems. Every production run is cataloged, and raw chips are retained for 24 months. We issue a comprehensive Certificate of Analysis (COA) specifying Delta E variance (≤ 0.5), Melt Flow Index (MFI), and moisture percentage per lot.
Yes. While virgin PE and PP are our primary volume carriers, our compounding lab develops specific carriers tailored for engineering resins (ABS, PS, PA, PC) and compostable matrices (PLA/PBAT) to eliminate interfacial delamination and mechanical embrittlement.
We operate under standard Incoterms 2020: FOB (Shanghai/Ningbo), CIF, CFR, and DDP to major international industrial corridors. We supply complete commercial documentation packages: Form E/Certificate of Origin, REACH/RoHS compliance statements, full GHS-compliant SDS, and third-party inspection certifications (SGS/TÜV).
Explore high-performance color solutions backed by twin-screw compounding stability, high pigment load efficiency, and non-bleeding chemical profiles.